Understanding Automatic Bag Palletizer Machines
In today's fast-paced manufacturing and logistics environments, efficiency is paramount. Automatic bag palletizer machines serve as a crucial technology in optimizing the final stages of production and packaging. These machines streamline the process of stacking bags onto pallets, freeing human workers from repetitive tasks and significantly enhancing productivity. With the ability to handle various bag sizes and materials, an automatic bag palletizer machine is an essential investment for businesses aiming to stay competitive.
What is an Automatic Bag Palletizer Machine?
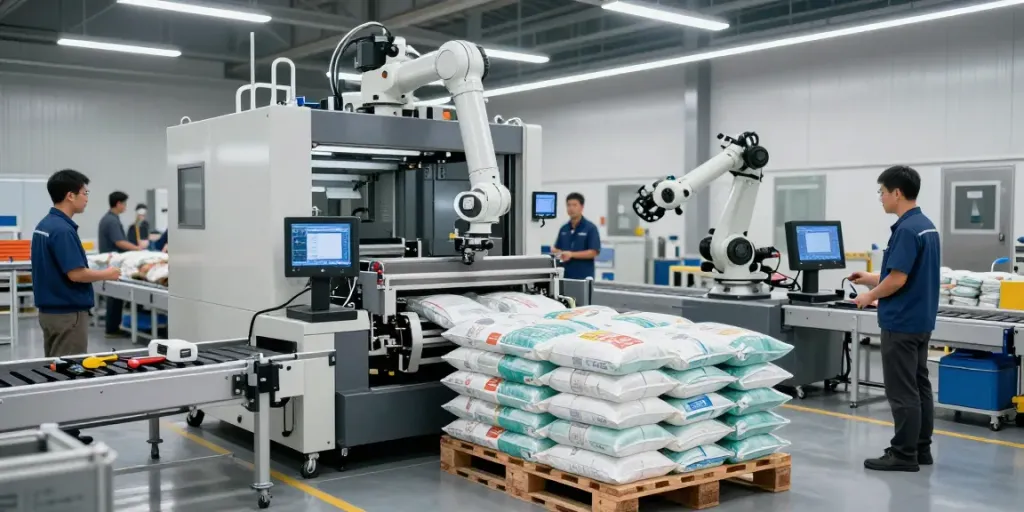
An automatic bag palletizer machine is an automated device designed to stack bags onto pallets with precision and speed. These machines are equipped with advanced robotics and software that enable them to identify bag sizes and orientations accurately, ensuring a stable and uniform pallet load. Commonly used in industries such as food, chemicals, and packaging, these machines can handle various bag types, from woven polypropylene to paper.
The Benefits of Implementing Automation in Your Operations
Integrating an automatic bag palletizer into your production line has several key benefits:
- Increased Efficiency: Automation significantly speeds up the palletizing process. Machines can handle dozens of bags per minute, far exceeding human capabilities.
- Improved Safety: Reducing manual handling of heavy bags decreases the risk of workplace injuries.
- Consistency and Quality Control: Automatic systems ensure uniform stacking and minimize the chances of human error, leading to higher quality pallet loads.
- Cost Savings: By automating repetitive tasks, companies can reduce labor costs and reallocate human resources to more strategic areas of the business.
Key Features to Look for in an Automatic Bag Palletizer
When selecting an automatic bag palletizer, consider these essential features:
- Flexibility: Look for machines that can accommodate various bag types, weights, and sizes.
- User-friendly Interface: An intuitive control system makes operation and troubleshooting straightforward, reducing training time for staff.
- High Throughput: Choose models that maximize speed without compromising on quality.
- Integration Capabilities: Ensure the palletizer can smoothly work alongside existing machinery in your production line.
Common Challenges and Risks
While automatic bag palletizers offer numerous advantages, businesses should also be aware of potential challenges that may arise during implementation and operation.
Identifying Operational Risks with Bag Palletizers
Like any automated system, bag palletizers come with risks that need to be proactively managed. Common operational risks include:
- Equipment Malfunction: Mechanical failures can cause production delays and increase maintenance costs.
- Safety Hazards: If not properly implemented, automated systems can pose safety risks to workers, especially in high-speed environments.
- Dependence on Technology: Relying heavily on automated systems can lead to vulnerabilities in case of system failures or software issues.
Addressing Integration Challenges with Existing Systems
Integrating a new automatic bag palletizer into existing production lines can be complex. Considerations include compatibility with current equipment and workflow processes. It's essential to conduct a thorough assessment of your existing systems and plan the integration carefully to minimize disruption.
Maintaining Safety Standards in Automated Environments
To safeguard employees working near palletizing machines, adhere to strict safety standards and protocols. Regular training sessions on safe operation and emergency procedures are crucial in minimizing risks associated with automated machinery.
Best Practices for Using Bag Palletizer Machines
To maximize the return on your investment in an automatic bag palletizer, following best practices is vital for operation and maintenance.
Regular Maintenance and Upgrades
Regular maintenance is crucial to keep your bag palletizer operating at peak efficiency. Schedule routine inspections and servicing to prevent mechanical failures. Additionally, consider upgrading software and hardware components as needed to keep pace with industry advancements.
Training Your Team for Optimal Operation
Your operators should receive comprehensive training on the specific palletizer model used in your facility. Understanding the machine's functions, potential issues, and standard operating procedures enhances safety and efficiency.
Effective Troubleshooting Techniques
Instill a culture of proactive problem-solving among your team. Encourage staff to recognize and report issues early, empowering them with troubleshooting techniques that can quickly restore operation and minimize downtime.
Real-World Applications and Success Stories
Automatic bag palletizers have transformed various industries by improving efficiency and product handling.
Case Study: Transforming Productivity in the Food Industry
In a leading food processing facility, implementing an automatic bag palletizer resulted in a 50% increase in throughput. By automating the palletizing process, the company reduced its reliance on manual labor and enhanced operational safety, leading to fewer workplace injuries and lower insurance costs.
Success in Packaging and Logistics: An Industry Overview
Across the logistics sector, companies have reported substantial improvements in order fulfillment speeds thanks to automated bag palletization. The ability to quickly and consistently palletize large volumes of products has streamlined shipping operations, minimizing delivery times and enhancing customer satisfaction.
How Different Industries Benefit from Automation
From chemicals to agriculture, the benefits of automatic bag palletizers extend across various sectors. Each industry experiences tailored advantages, such as:
- Agriculture: Efficient handling of bulk feed and fertilizers.
- Chemicals: Safe movement of hazardous materials with reduced manual handling.
- Retail: Streamlined packaging and palletizing processes for various retail products.
Future Trends in Automatic Bag Palletizing
The landscape of automatic bag palletizers is continually evolving, driven by technological advancements and changing market demands.
Technological Innovations on the Horizon for 2026
As we look to the future, expect innovations like enhanced robotics capabilities, real-time monitoring systems, and improved energy efficiency. These advancements will further reduce costs and increase the productivity of palletizing operations.
The Impact of Artificial Intelligence in Palletizing
Artificial intelligence (AI) is set to revolutionize automatic bag palletization through smarter systems that learn and adapt to production requirements. This technology can optimize stacking patterns in real time, improving load stability and reducing waste.
Preparing for Future Challenges in Automation
With advancements come challenges related to cybersecurity and technology adoption. Companies must invest in training and infrastructure to ensure their workforce can adapt to new technologies while safeguarding against potential threats.
What are the key benefits of an automatic bag palletizer machine?
The benefits include increased production speed, improved safety, enhanced consistency in pallet loads, and significant cost savings through reduced labor needs.
How does automation improve workflow efficiency?
Automation streamlines processes, minimizes manual handling, and optimizes labor allocation, allowing businesses to focus on core operations while maintaining high throughput levels.
What maintenance is needed for bag palletizer machines?
Regular maintenance should include inspections, cleaning, lubrication, and software updates to ensure machines operate efficiently and safely.
What industries can benefit from bag palletizers?
Industries such as food processing, chemicals, agriculture, and logistics can all benefit from the efficiencies gained through automatic bag palletization.
How can I customize bag palletizing solutions for my business?
Consult with a reputable supplier to explore customization options, ensuring your palletizer meets specific production requirements and integrates seamlessly with existing workflows.